


 Business License
Blog Categories

Barrel Electroplating for Metal Buttons: How the Line Works
Metal buttons are coated in bulk rather than one at a time, and the reason is commercial as much as technical. A Barrel Plating Button line tumbles thousands of small parts in a rotating cylinder that is lowered into each tank in turn, which keeps the labour per part low and the coating even across a large batch.
This article follows a batch through the whole cycle, from loading and degreasing to the final rinse and dry. It sets out the Electroplating Button Process in the order it happens on the floor, then explains the settings that are controlled and the checks that decide whether a Metal Button Plating Line is still holding to its specification.
1. What a Barrel Plating Button Line Does
A Barrel Plating Button line exists because small parts cannot be hung on a jig economically. An operator would spend longer attaching a rivet to a wire than the coating on that rivet is worth, so the parts are loaded loose into a perforated barrel and electrical contact arrives through a flexible cable that touches the tumbling load.
The barrel turns slowly, usually between 3 and 12 revolutions per minute, and the rotation does three jobs at once. It keeps the parts moving so that no face stays pressed against another part, it helps the solution reach every surface, and it stops one contact point from carrying the whole current.
The trade is that barrel work is slower per part and kinder to the surface than rack plating. Small trim parts with no flat display face are the natural fit, which is why Difei Button coats snaps, rivets, eyelets and jeans button caps in barrels and keeps rack work for badges that need a clean front.
2. The Electroplating Button Process Step by Step
The Electroplating Button Process runs through a fixed sequence of tanks, and each tank does a job that the next one depends on. Skip a step and the coating will still form, but the adhesion and the colour become unpredictable, which is the kind of fault that appears after shipment rather than before it.
The sequence opens with a soak clean that removes the oil left by stamping, followed by an electroclean that lifts the last film, then two counterflow rinses. Acid activation comes next to expose fresh metal, and the barrel must enter the plating tank within a short window so that the active surface does not oxidise.
After plating, the barrel passes through a drag out rinse, a neutralising dip and two more rinses before a hot air dry. The drag out tank is not a formality, since it captures carried over solution and returns it to the plating tank, which saves chemistry and reduces what leaves in the rinse water.
3. Metal Button Plating Line Layout and Tank Sequence
A Metal Button Plating Line is laid out as a row of tanks with a travelling hoist above them, and the layout decides how quickly a batch can move. Short travel between tanks reduces drip time, while travel that is too short carries more solution into the next tank than the rinse can absorb.
A typical line holds ten to fourteen stations for one coating: load, soak clean, electroclean, rinse, rinse, activate, rinse, plate, drag out, neutralise, rinse, rinse, hot dry and unload. Where two coatings are applied in sequence, such as nickel beneath tin, the run repeats from the activation stage with a second plating tank in the same row.
Tank volume matters for consistency. A 600 litre plating tank can carry a barrel load of 40 to 60 kg of small buttons, and the ratio of load to volume is what keeps the metal ion concentration from falling quickly. When the load is increased without the volume, the deposit thins towards the ends of the batch.
4. Barrel Plating Button Chemistry: Nickel, Tin and Zinc
A Barrel Plating Button bath is chosen for the finish the buyer asked for and for the corrosion life the end use requires. Nickel gives a bright, hard deposit with a warm grey tone, tin gives a soft matte look that forms and solders easily, and zinc gives a low cost barrier that is usually finished with a clear passivation.
Three coating systems account for most metal trim. Bright nickel from a Watts bath runs at 50 to 60 degrees Celsius, acid tin runs near room temperature, and alkaline zinc runs at 25 to 35 degrees. Copper and brass serve as undercoats or as an antique finish, and a trivalent chrome passivation produces a dark tone without the hazards of hexavalent chemistry.
Thickness is set by the end use rather than by the tank. Decorative trim on a jacket usually carries 2 to 5 microns of nickel, hardware that faces salt spray testing carries 8 to 12 microns, and a zinc layer of 5 to 8 microns supports the passivation that resists white rust on a humid journey.
5. Electroplating Button Process Control: Current and Time
The Electroplating Button Process is controlled through four settings, and the deposit thickness is the result of all four acting together. Current, time, temperature and barrel rotation are recorded for every batch, because a change in any one of them moves the result even when the chemistry is unchanged.
| Setting | Usual range | Effect when it drifts |
|---|---|---|
| Current density | 0.5 to 2 A per square decimetre | Thin or burnt deposit |
| Time in the tank | 15 to 45 minutes | Thickness moves off target |
| Bath temperature | 50 to 60 degrees Celsius | Grain size and brightness change |
| Barrel rotation | 3 to 12 revolutions per minute | Dull patches or a matte coat |
Current density in a barrel is lower than on a rack, since the load shades itself. A working figure for nickel is 0.5 to 2 amperes per square decimetre of surface area, and the surface area of a load is calculated from the part count and the coated area of a single part. Time is then set from the current density using the deposit rate of the metal.
Rotation speed is the setting most often left alone and most often worth changing. Too slow and the parts sit in contact, which leaves a dull patch where no current reached. Too fast and the load turns over so quickly that contact becomes intermittent, which gives a thin deposit with a matte appearance. Difei sets rotation from the size and weight of the part rather than from a house number.
6. Metal Button Plating Line Maintenance and Bath Analysis
A Metal Button Plating Line stays in specification through analysis rather than through experience, and the schedule is short. Temperature, pH and specific gravity are checked at the start of every shift, and the full metal content with the additive level is checked once a day.
Four tasks keep a line stable. Anode bags are inspected for rupture every week, the filter is changed on the hours the supplier states, the barrels are checked for a cracked panel that would let parts escape, and the contacts are replaced when the surface pits. None of the four costs much, and each one prevents a fault that would otherwise reach a finished shipment.
Bath life is finite, and the decision to treat or to replace is taken on analysis. Carbon treatment removes organic contamination, a dummy plate removes metallic impurities, and the bath is replaced when the additive balance can no longer be restored. A line that logs every analysis can show a buyer the history behind a coating specification.
7. Barrel Plating Button Quality Checks and Testing
A Barrel Plating Button batch is checked on four properties before it leaves the plating area: coating thickness, adhesion, appearance against the approved sample, and corrosion resistance where the end use calls for it. Results are filed against the batch number rather than the order number, so that a question about one delivery can be answered from a record that covers a single run.
Thickness is read on a magnetic gauge at three points across several parts, since a barrel produces a range across the load rather than a single figure. Adhesion is checked by bending a coated part over a radius and looking for lifting or flaking at the bend, and appearance is judged against the sample under a fixed light rather than under whatever the workshop ceiling provides.
Corrosion testing takes longer. A neutral salt spray test runs for 24, 48 or 72 hours and is reported as the time to first white rust and to first red rust. Difei Button keeps the test panels from every batch, so a buyer can compare the paper report with the physical evidence at any point in the season.
8. Electroplating Button Process and Environmental Control
The Electroplating Button Process produces rinse water, spent bath and filter sludge, and the way a line handles those three streams separates a compliant workshop from one that will be closed by an inspection. The controls needed are ordinary engineering rather than specialised chemistry.
Three practices carry most of the load. Counterflow rinsing cuts the volume of rinse water, an ion exchange unit returns metal from the rinse stream, and the plating area sits on a bunded floor so that a spill cannot reach a drain. Sludge and spent baths go to a licensed treatment contractor with every transfer recorded.
Record keeping is part of the control. Manifests, water meter readings and analysis logs show that a line was operated inside its permit, and they also support the material declarations a buyer needs for a restricted substances file. A supplier that can produce those documents is easier to audit than one that can describe its process but not prove it. Difei Button (Guangzhou) Co Ltd plates, inspects and files those records in the same building, so an audit can follow a batch from the barrel through to the packing list without leaving the site.
9. Frequently Asked Questions
9.1 What is barrel plating and why is it used for buttons?
Barrel plating is a bulk method in which loose parts tumble inside a perforated cylinder that is lowered into each tank in turn. Contact arrives through a flexible cable that touches the moving load, so thousands of small buttons can be coated in one cycle without an operator attaching each one to a wire. The rotation keeps the parts moving so that no face stays hidden and no single contact point takes the whole current. It suits snaps, rivets, eyelets and jeans button caps, which have no flat display face that has to stay unmarked.
9.2 How thick is the plating on a metal button?
It depends on the end use rather than on one house figure, so the target should be written into the specification that the Metal Button Plating Line works to. Decorative trim on a jacket usually carries 2 to 5 microns of nickel, while hardware that faces salt spray testing carries 8 to 12 microns. A zinc layer of 5 to 8 microns supports the passivation that resists white rust during a humid sea journey. The plating ticket then states the target, the tolerance and the test that proves the figure after each batch.
9.3 What controls the thickness in a plating barrel?
Four settings act together in the Electroplating Button Process, and no single one of them sets the result on its own. Current, time, temperature and barrel rotation are recorded for every batch, because a change in any one of them moves the deposit even when the bath chemistry is unchanged. Current density in a barrel is lower than on a rack because the load shades itself, and a working figure for nickel is 0.5 to 2 amperes per square decimetre. Rotation speed matters as well, since a barrel that turns too slowly leaves a dull contact patch and one that turns too fast gives a thin matte deposit.
9.4 How is plating quality checked before shipment?
Four properties are checked before a Barrel Plating Button batch leaves the plating area. Thickness, adhesion, appearance against the approved sample, and corrosion resistance where the end use calls for it, with every result filed against the batch number. Thickness is read on a magnetic gauge at three points across several parts, because a barrel produces a range across the load rather than one figure. Corrosion is measured by a neutral salt spray test running for 24, 48 or 72 hours, reported as the time to first white rust and to first red rust.
Recently Posted
-
When Something Goes Wrong: How Difei Button Handles Claims and Rework
October 16, 2026A trim defect found at the sewing line costs more than the trim. The line stops, the operator is paid to wait and the delivery dat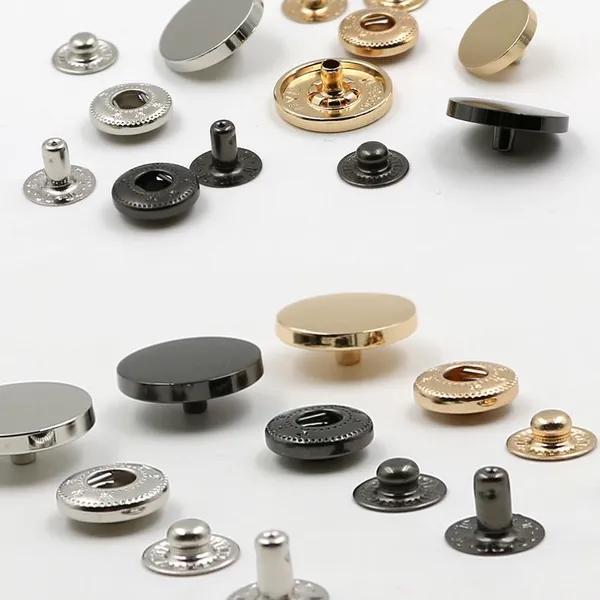 Read More
-
Automated Inspection in Button Production: Vision and Sorting
October 16, 2026A button is small, low in value and produced in millions, which makes it a poor candidate for hand inspection and a good one for a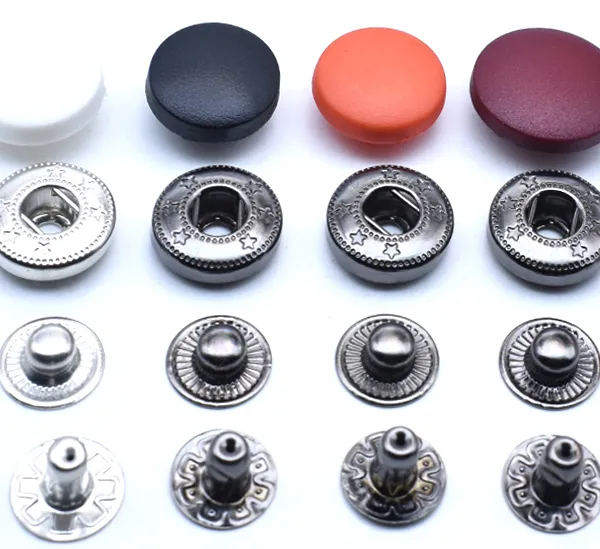 Read More
-
Air vs Sea Freight for Trim Orders: Planning Delivery Dates
October 16, 2026Trim is the last material to arrive and the first to stop a sewing line, which is why the calendar rather than the rate usually de Read More
-
Inspecting Mixed Trim Shipments: Buttons, Rivets and Eyelets Together
October 16, 2026A trim order rarely arrives as one product. A single container usually carries snaps, rivets, eyelets, jeans buttons and badges, p Read More

Contact Us
Recommended Products
-
 Clothing Accessories Lead Free Brass Metal Ring Prong Snap Button With 4 Parts for Infant Baby Clothes Baby BibsUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Brass Metal Stainless Steel Material Ring Prong Snap Button With 4 Parts Lead Free & Nickel Free for Infant Baby Clothes Baby Bibs Baby SuitsUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Metal Grommets Eyelets Gold Eyelet for Bag Shoes and Garment AccessoriesUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Cheap Price Custom Jeans Button Metal Custom Logo Metal Button for JeansUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Factory Wholesale Hat Bag Clothing Press Snap Button Spring Snap Button Metal Snap ButtonsUS$ 0.03 - 0.06MOQ: 5000 Sets




-
Wholesale Plastic Round Coloured Snaps Button Press Fasteners for Baby Bibs/ Baby GarmentsUS$ 0.01 - 0.03MOQ: 50000 Sets
-
Custom EngravedCopper I Brass Metal Jeans Button Denim Clothes Jacket for Jeans DenimUS$ 0.01 - 0.03MOQ: 5000 Sets
-
17mm Open Hole Shank Button With Aluminum Nail With Logo for Jeans Jacket PantsUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Eco-friendly Custom Size Plastic Snaps Plastic Snap Button for Baby Clothes, Baby BibsUS$ 0.01 - 0.03MOQ: 50000 Sets
-
12mm 15mm 17mm 20mm Four Parts Metal Brass Fastener Press Snap Button for Clothes JacketUS$ 0.03 - 0.06MOQ: 5000 Sets





-
Custom Logo Personalized High Quality Metal Press Snap Fastener Snap Buttons for Clothing Garments JacketUS$ 0.03 - 0.06MOQ: 5000 Sets
-
Custom Printing Round Press Spring Four Part Snap Button for Clothing Leather 405#17mmUS$ 0.03 - 0.06MOQ: 5000 Sets
-
OEM Garment Accessories Custom Baby Snap Button Press Metal Prong Pearl Ring Snap ButtonUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Factory Stock Buttons Stainless Steel or Brass Material Colors Pearl Snap Button Prong Pearl Snap Button for Shirts ClothingUS$ 0.01 - 0.03MOQ: 5000 Sets
-
Apparel Hardware 222# Cap Prong Ring Snap Fastener 10mm for Coat FasteningNegotiableMOQ: 50000 Pieces





-
Open Hole Prong Ring Snap Button 222# 10mm for Leather Sewing ProjectsNegotiableMOQ: 50000 Pieces
-
Zinc Alloy 222# 10mm Open Hole Prong Ring Snap Button Wholesale for Clothing Factory UseNegotiableMOQ: 50000 Pieces
-
222# 10mm Open Hole Prong Ring Snap Fastener for Clothing Sewing and LeatherNegotiableMOQ: 50000 Pieces
-
Antique Bronze 222# 10mm Open Hole Cap Prong Ring Snap Buttons for Denim and Canvas GarmentsNegotiableMOQ: 50000 Pieces
-
New Style 222# 10mm Snap Buttons Cap Type for Bag DecorationNegotiableMOQ: 50000 Pieces





